

 English
 Español
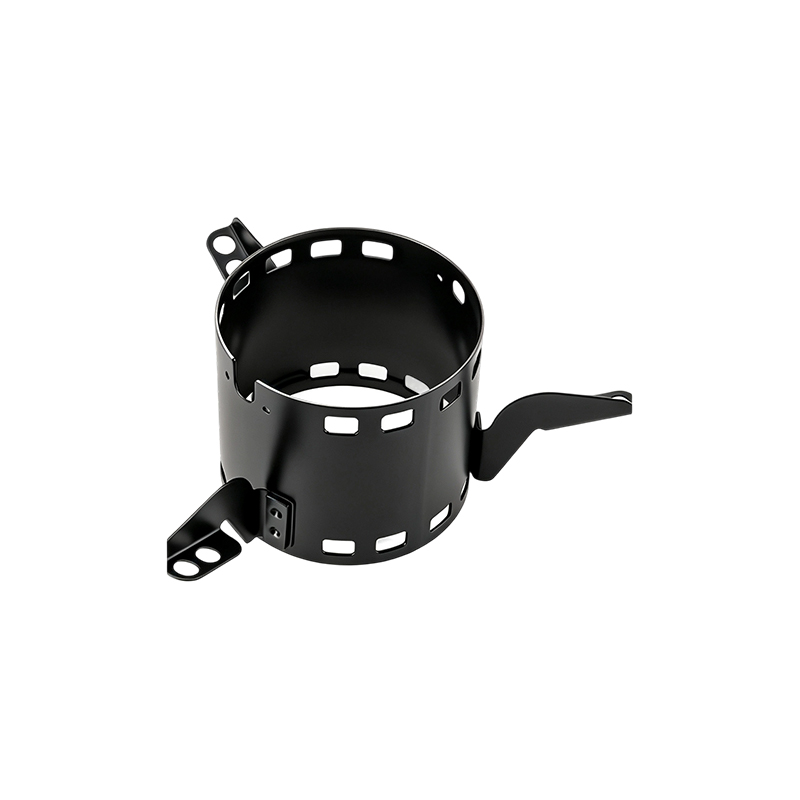
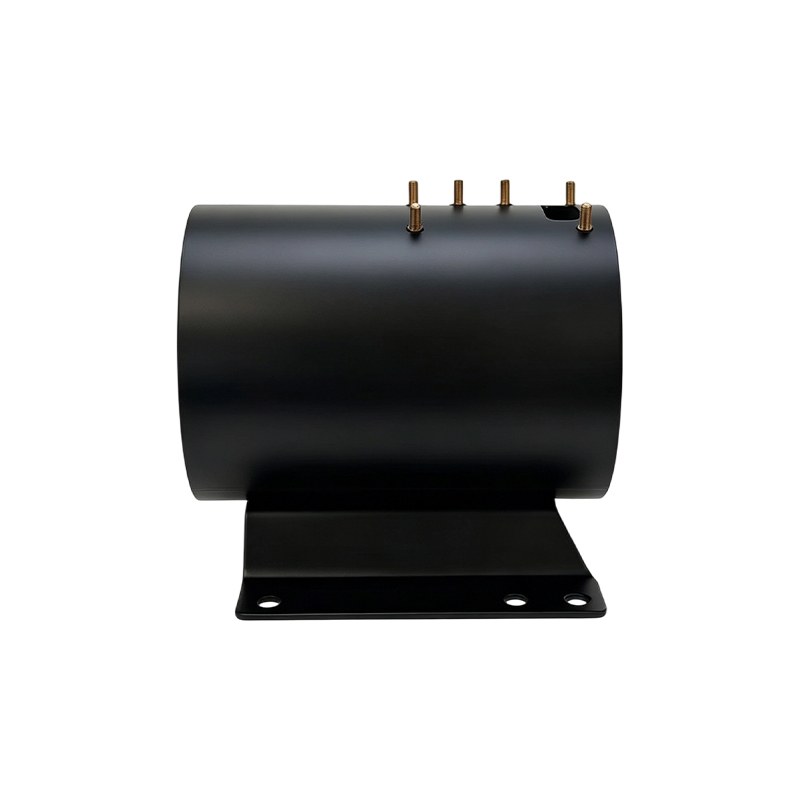
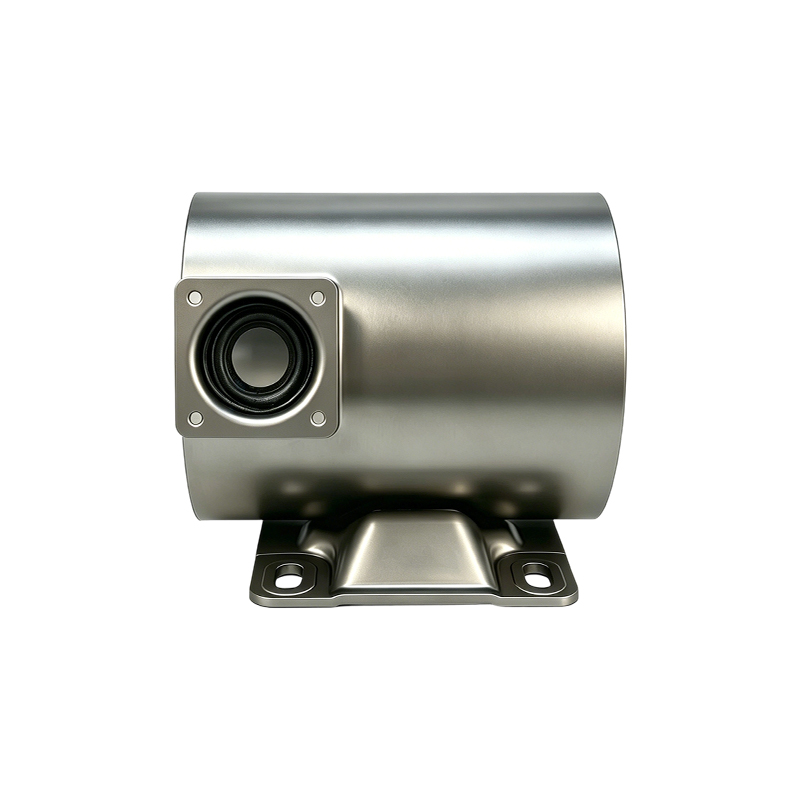
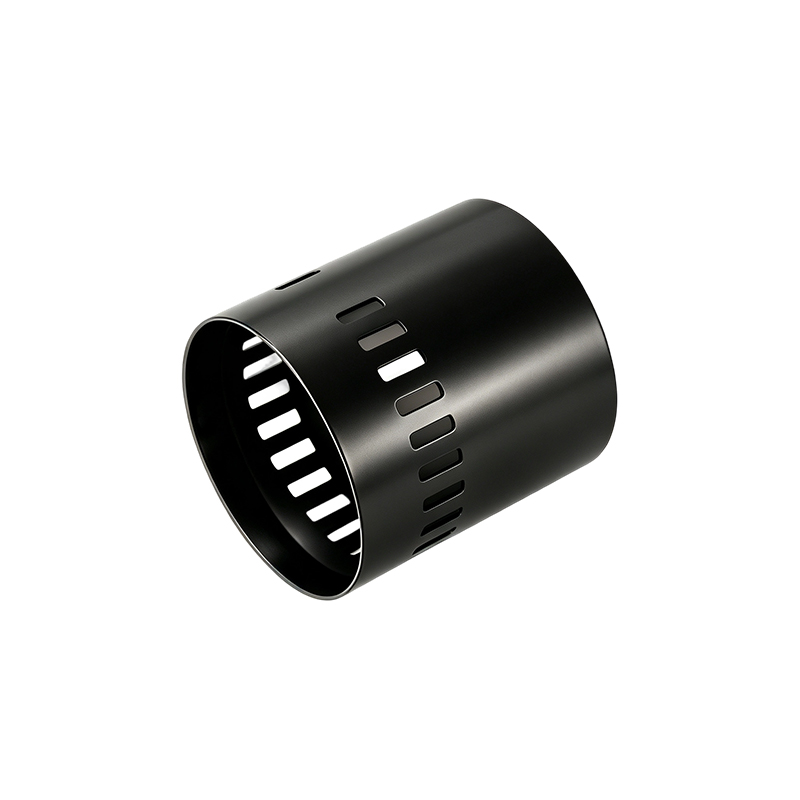
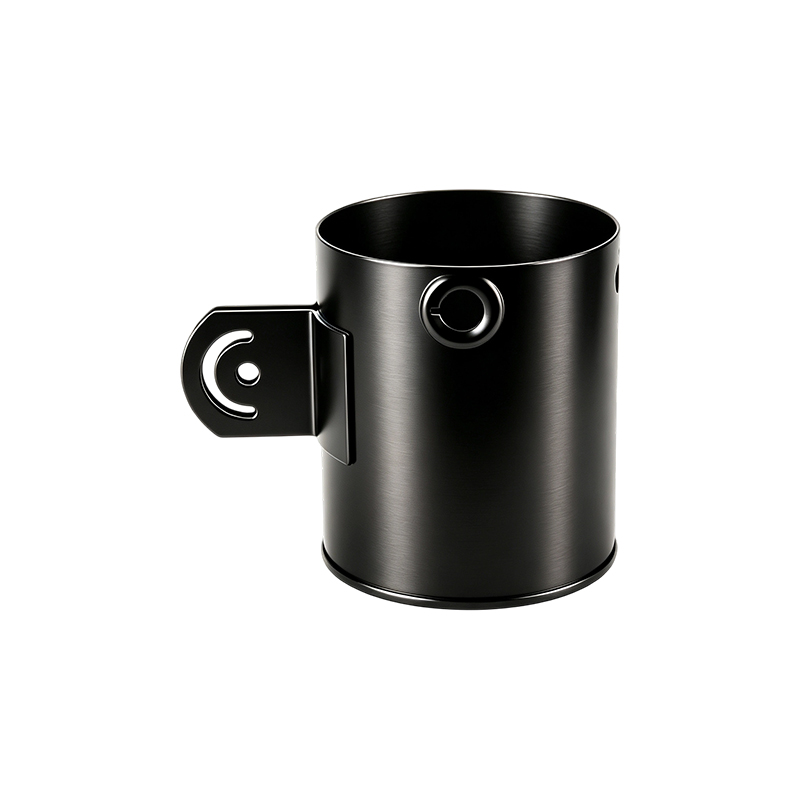
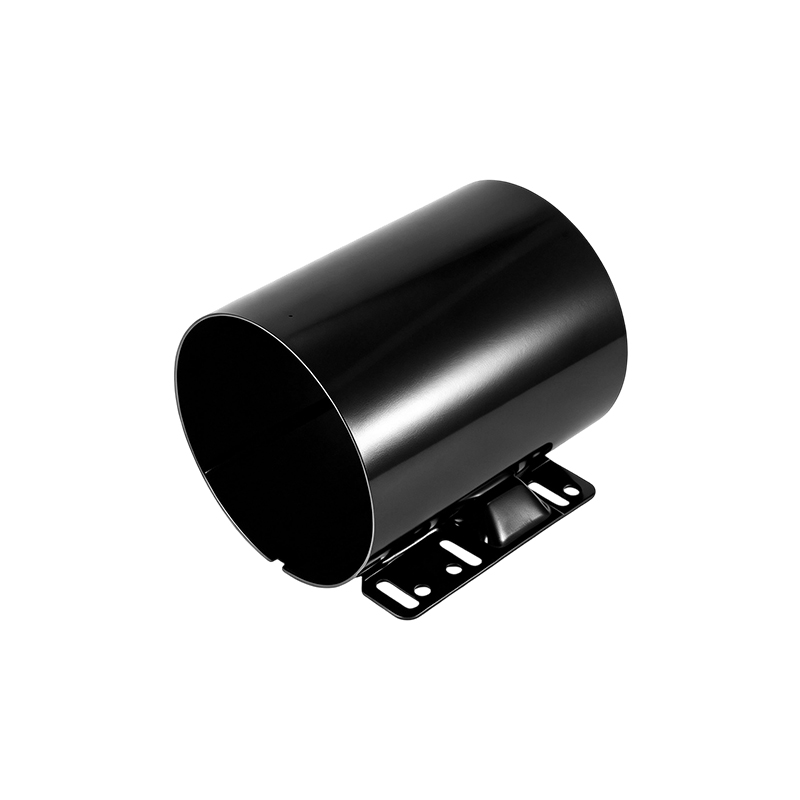
Thin-Wall EV Traction Motor Stators
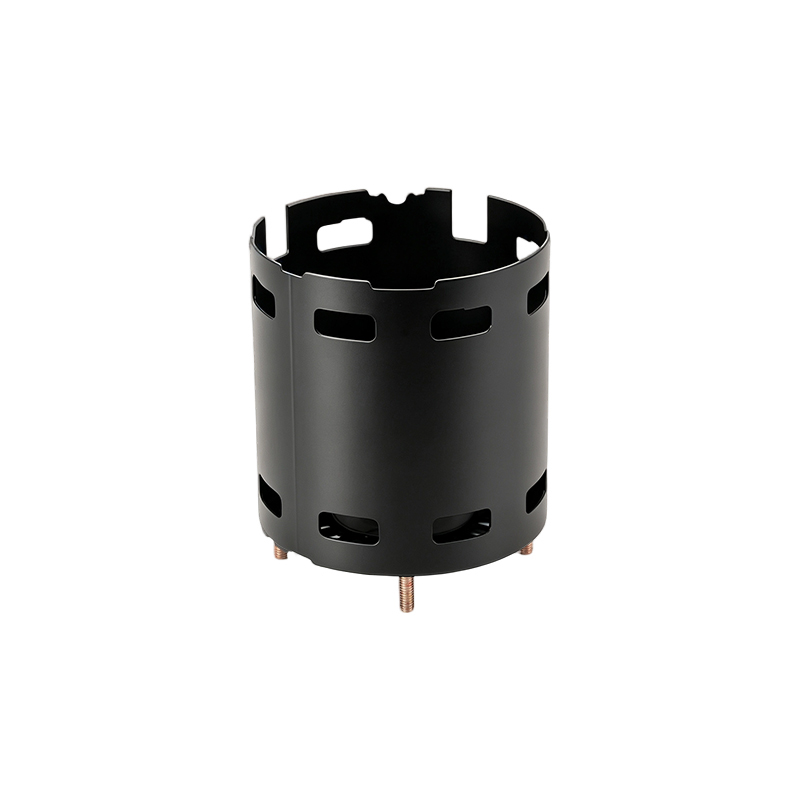
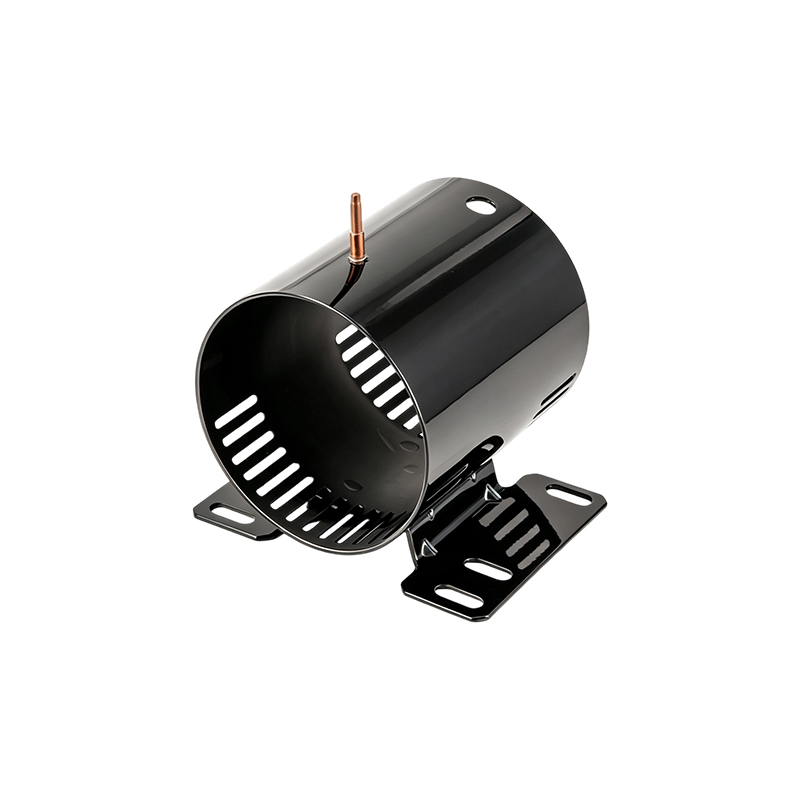
Thin-wall stator housings for electric vehicle traction motors, where reduced wall section supports weight reduction while maintaining the roundness and dimensional stability needed for stator lamination stacking, winding, and rotor clearance. Manufactured by Jiangsu Yufeng Electric Co., Ltd. through integrated stamping, automated welding, precision machining, and in-house coating processes.
A thin-wall EV traction motor stator housing must hold a precise internal diameter through the full assembly sequence, because stator lamination stack concentricity and rotor air gap both depend on it. Reducing wall thickness saves mass, but it also lowers stiffness and increases sensitivity to weld distortion, clamping force, and thermal expansion. The housing therefore has to be designed and manufactured so that the thin section remains round after welding, machining, and coating.
Jiangsu Yufeng Electric Co., Ltd. produces these stator housings with continuous stamping for material utilization above 92 percent, automated welding for repeatable seams, and precision machining on bore and mounting features. Coolant jacket interfaces and end face geometry are machined to drawing requirements, and key dimensions are checked with custom gauges and online inspection equipment.
Material Utilization
Continuous stamping reaches above 92 percent utilization, which supports cost control on volume traction motor programs.
Wall Section Control
Wall thickness and roundness are managed through forming and welding so the thin section holds its geometry after coating.
Bore And Fit Accuracy
Bore and end face features are machined and checked with custom gauges to support stator stacking and rotor clearance.
Process Control
ISO 9001:2015 quality system, with IATF 16949 aligned process control and traceability for automotive customers.
Production Capability
Design And Manufacturing Points
- Thin Section Forming Wall thickness is controlled during continuous stamping so the thin section keeps uniform thickness around the circumference. This reduces the risk of local thinning that would lower stiffness and distort the bore after welding.
- Weld Distortion Control Automated welding produces repeatable seam geometry, and weld sequencing is managed so that heat input stays consistent. This limits ovality that would otherwise appear in a thin-wall housing after joining.
- Bore Machining Internal bore and end face features are machined after welding rather than before, so final concentricity and squareness reflect the joined housing instead of the pre-weld shell.
- Coolant Jacket Interfaces Coolant jacket connection features are machined to drawing requirements, with position and sealing face geometry checked so that the interface supports leak-free assembly.
- Surface Treatment Electrophoretic coating and powder coating are applied on in-house lines. Coating selection considers coolant exposure, road splash, and the electrical insulation requirements of the traction system.
- Traceability Each batch is traceable to raw material lots, production machines, and operators. This supports fast identification when a dimensional deviation appears and enables closed-loop corrective action.
Product Specifications
| Base Material | Steel, stainless steel, and other specified metals selected for traction motor housing requirements |
| Wall Construction | Thin-wall formed shell with controlled thickness distribution around the circumference |
| Welding | Automated welding with managed heat input to limit distortion in the thin section |
| Bore Machining | Internal bore and end face machined after welding for concentricity and squareness |
| Coolant Interface | Jacket connection features machined to drawing requirements for sealing face geometry |
| Forming | Continuous stamping with material utilization above 92 percent |
| Surface Treatment | Electrophoretic coating and powder coating on in-house lines |
| Inspection | Custom gauges and online inspection equipment on key dimensions |
| Quality System | ISO 9001:2015; IATF 16949 aligned process control for automotive customers |
| Customization | Bore diameter, wall section, coolant interface, mounting features, and coating adapted to motor design |
Application Scenarios
Passenger EV Traction Motors
Stator housings for passenger electric vehicle drive units where mass reduction and bore accuracy both affect efficiency and noise.
Commercial Vehicle Drive Units
Housings for electric buses and light commercial vehicles that combine higher continuous load with weight targets.
Integrated E-Axle Assemblies
Stator housings for integrated motor and gearbox units, where housing roundness affects gear mesh and bearing alignment.
Hybrid Powertrains
Housings for hybrid drive motors that operate across stop-start and continuous duty cycles with thermal cycling.
Electric Off-Highway Equipment
Stator housings for electrified construction, agriculture, and material handling equipment exposed to vibration and dust.
High-Speed Traction Motors
Housings for high-speed traction designs where bore concentricity supports rotor clearance at elevated speed.
Frequently Asked Questions
A thin-wall housing uses a reduced wall section to lower mass, which also lowers stiffness. That makes the housing more sensitive to weld distortion, clamping load, and thermal expansion, so bore roundness and concentricity must be controlled after joining rather than assumed from the pre-weld shell.
Welding is performed with automated equipment and managed heat input to limit distortion. The internal bore and end face are then machined after welding, so final concentricity reflects the joined housing. Key dimensions are verified with custom gauges and online inspection equipment.
Electrophoretic coating and powder coating are applied on in-house lines. Selection considers coolant exposure, road splash, and the insulation requirements of the traction system.
Yes. Bore diameter, wall section, coolant jacket interface, mounting features, and coating can be adapted to the motor design. Changes are handled through in-house tooling design and process parameter optimization.
Standard non-standard custom samples can be delivered within 3 to 10 working days. Complex custom projects can complete first-article samples within 15 days.
Product drawings or detailed specifications, including bore diameter, wall thickness, material, coolant interface requirements, surface treatment, estimated annual demand or quantity per batch, and any special technical requirements. Quotations are typically provided within 2 to 3 working days after confirmation.
Yes. Multi-variety and small-batch manufacturing is supported, covering development trials, small-to-medium volume orders, and flexible multi-batch scheduling as a traction motor program moves toward mass production.
Selection Notes
Bore And Wall Section
Define bore diameter, wall thickness, and roundness tolerance against the stator lamination stack and rotor air gap requirement.
Coolant Interface
Specify jacket connection geometry and sealing face requirements so the interface supports leak-free assembly with the cooling circuit.
Coating And Insulation
Confirm coating type and thickness against coolant exposure, road splash, and the electrical insulation requirements of the drive system.
Thermal And Mechanical Load
Review wall section against thermal cycling and vibration load, since a thin wall responds differently than a conventional housing.
Traceability Scope
Define batch traceability requirements for raw materials, production processes, and finished product inspection records.
Order Planning
Provide estimated annual demand and batch size so production planning and cost optimization align with program milestones.
Manufacturing Solutions
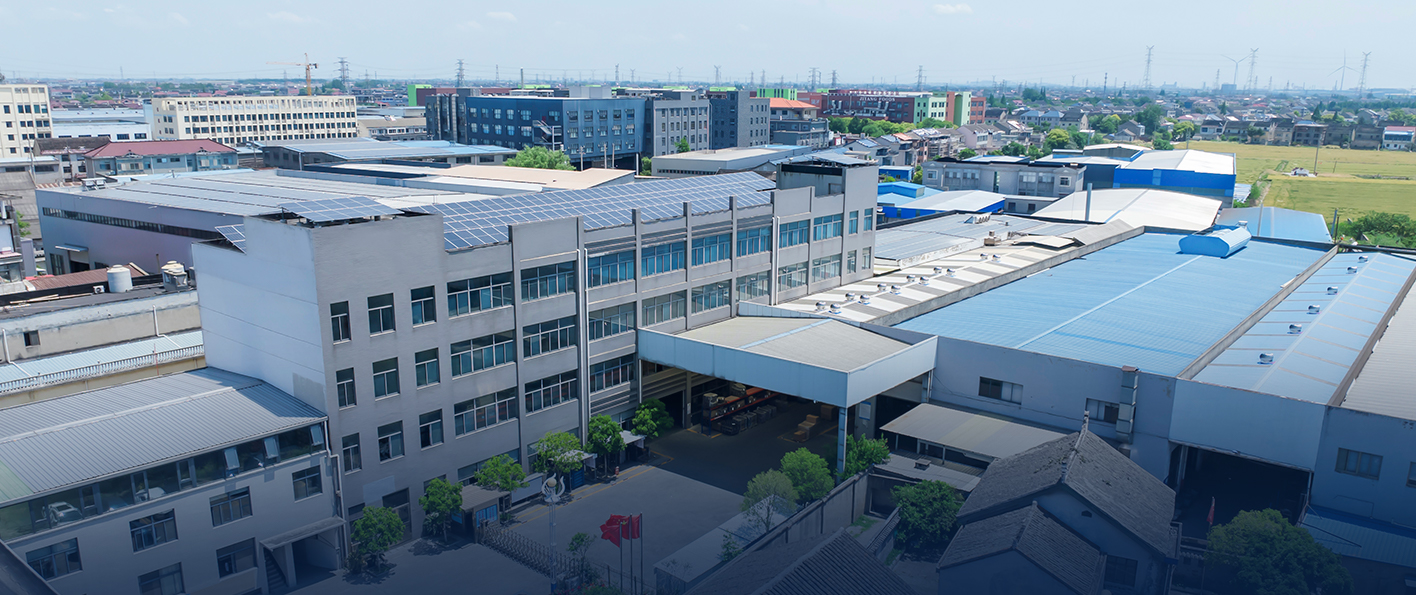
We offer full-process manufacturing capabilities from steel processing to finished product delivery, supported by stamping lines, automated welding equipment, machining facilities, and inspection instruments. Backed by an engineering team with an average of over 20 years of experience, we provide technical support from development to mass production.
With 40 years of focus on motor housing manufacturing, we have served more than 50 customers and achieved an annual production capacity of over 5 million units. Guided by quality, efficiency, and fast response, we are committed to delivering high-precision and high-reliability motor housing solutions.